Centerless Ground Stainless Steel Bar: h9 Tolerance, Inspection and CNC Buying Guide
A procurement guide to centerless ground stainless steel bar for CNC shafts and pins, covering h9 size limits, straightness, roundness, inspection records and RFQ wording.
In This Guide
- Why starting-bar condition matters
- Quick answer
- What centerless grinding changes
- When h9 is useful for CNC parts
- Ground bar, cold-drawn bar and peeled bar serve different jobs
- H9 does not define the whole bar
- How to inspect diameter before shipment
- Check straightness, surface and bar ends separately
- Grade choice and traceability
- RFQ wording example
- Common buying mistakes
- Sources and scope
- Request a ground bar quotation
Why starting-bar condition matters
A CNC drawing may define the finished shaft precisely, yet the purchase order for raw bar says only stainless steel round bar. That gap can create avoidable work. Diameter variation affects collet grip and machining allowance. Poor straightness can disturb a bar feeder. Surface defects that remain after a light cut can appear on the finished part.
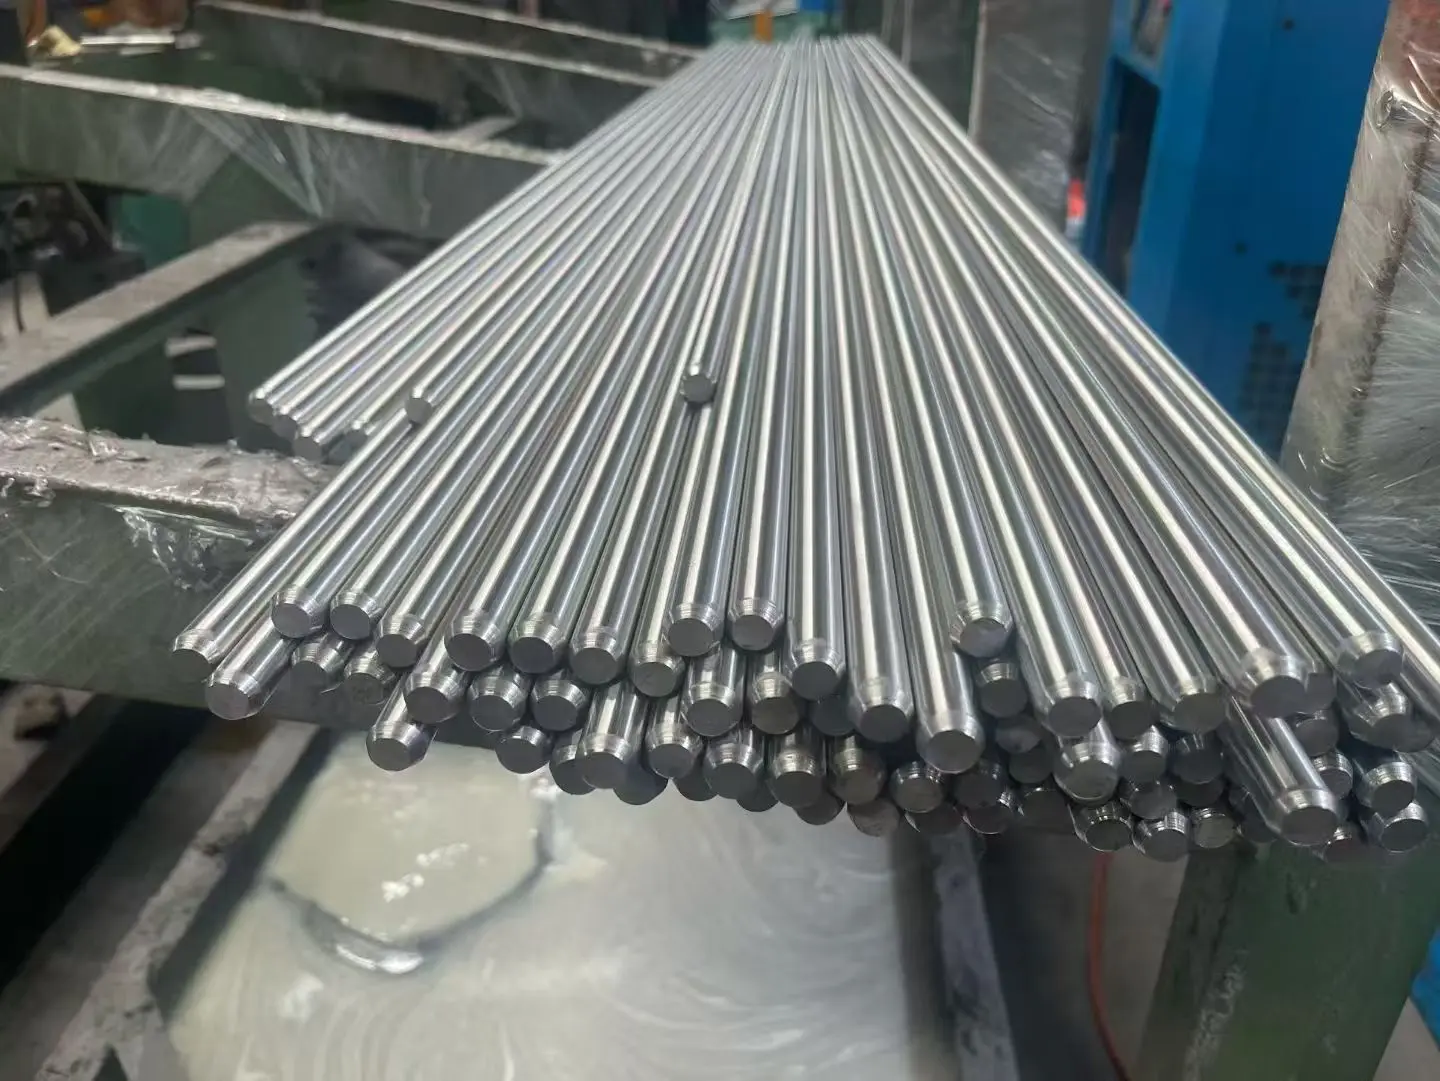
Centerless ground stainless steel bar addresses the outside diameter and surface before the material reaches the machine. It is useful when those starting conditions affect feeding, cycle stability or the amount of stock that must be removed. It is not automatically the right route for every turned part, and the word *ground* does not by itself prove h9 tolerance.
This guide focuses on purchasing and incoming inspection. For a full comparison of ISO size classes, use the separate h9, h10 and h11 stainless steel bar tolerance chart.
Quick answer
Order centerless ground stainless steel bar when a CNC shaft, pin or bar-fed part needs a controlled starting diameter, smooth cylindrical surface and repeatable condition from bar to bar. Put the nominal diameter and tolerance on the RFQ rather than asking only for “precision ground bar.”
Before shipment, check six items:
- nominal diameter and the exact h9 or drawing limits;
- measured diameter at agreed positions along the bars;
- straightness and roundness limits when the machine or finished part depends on them;
- surface roughness or visual acceptance where the ground surface remains on the part;
- grade, standard and heat number on the MTC and bundle labels;
- cut length, end condition, packing and identification for each bundle.
An MTC proves material identity and batch information. It does not replace the dimensional inspection record.
What centerless grinding changes
In centerless grinding, the round bar passes between a grinding wheel, a regulating wheel and a work-rest blade. Unlike cylindrical grinding between centers, the workpiece is supported externally and does not need to be held by centers. This route can process long round stock efficiently while improving diameter consistency and surface condition.
The result still depends on the starting bar, grade, diameter, bar length, straightening, grinding setup and agreed inspection method. Buyers should therefore purchase the measured result, not rely on the process name alone.
A centerless ground stainless steel bar inquiry should state the finished diameter after grinding. If the bar will receive another grinding or turning operation, also state the machining allowance needed by the customer’s process.
When h9 is useful for CNC parts
For an external dimension using the ISO shaft tolerance position h, the upper deviation is zero. The actual diameter may equal the nominal size but must not exceed it; the lower deviation depends on the nominal-size interval and tolerance grade.
For example, a 20 mm h9 shaft-size callout corresponds to 20.000 to 19.948 mm under ISO 286-2. A buyer ordering that size should not accept a generic statement such as “about 20 mm” or “bright bar tolerance.” The size window belongs on the quotation, purchase order and dimensional report.
H9 may be justified when:
- the bar feeds through a close collet or guide bush;
- the supplied surface remains on part of a shaft or pin;
- light machining leaves little allowance for diameter variation;
- repeat batches must enter the same CNC setup with limited adjustment;
- incoming sorting would cost more than purchasing a controlled bar route.
H9 is not automatically better. If the first operation removes substantial stock, h10, h11 or an explicit machining-allowance range may be sufficient. The stainless steel bar tolerance lookup can calculate common limits, but the drawing and named standard remain the acceptance basis.
Ground bar, cold-drawn bar and peeled bar serve different jobs
These terms describe processing routes, not interchangeable quality grades. The most economical choice depends on what the next operation needs.
| Supply Route | What the Buyer Receives | Typical Purchasing Use | Point to Put on the PO |
|---|---|---|---|
| Cold drawn / bright | Improved size consistency and surface compared with hot-rolled stock | General CNC turning and bar-fed production | Actual diameter tolerance; do not assume h9 |
| Peeled / turned | Outer scale and surface layer removed, commonly with allowance for further machining | Larger shafts, forging stock and heavier turning | Finished supplied diameter and remaining allowance |
| Centerless ground | Controlled cylindrical diameter and smoother ground surface | Shafts, pins, guide components and closer bar feeding | Diameter limits plus separate form and surface requirements |
| Hot rolled | Broader raw-stock route with more surface and size variation | Forging or parts receiving heavy machining | Machining allowance and defect-removal plan |
The general stainless steel round bar page compares these supply forms. Buyers should not pay for a ground route when the next operation removes the benefit, but they should not expect ordinary bright bar to satisfy an unstated precision requirement.
H9 does not define the whole bar
A bar can pass its h9 diameter limits and still cause trouble in production. Size, form, orientation and surface are separate characteristics. If any of the following matters, write it separately:
- Straightness: affects long rotating parts, guide bushes and bar feeders. State the permitted deviation and measurement basis.
- Roundness or ovality: affects how consistently different angular positions measure and contact a collet or bearing surface.
- Cylindricity: may matter when the supplied surface functions as a finished cylindrical feature.
- Surface roughness: matters when the ground surface remains visible or contacts a seal, bearing or mating part.
- Cut-length tolerance: affects automatic loading, fixed blanks and packing.
- End condition: saw-cut, chamfered or faced ends should be named when they affect loading or the first operation.
Do not write “h9 including straightness and roughness” as though one code covers everything. Give each critical characteristic its own value, standard or drawing note.
How to inspect diameter before shipment
A useful dimensional report connects the ordered limits to measured bars. A sheet containing one unexplained number is weak evidence, even if that number falls inside h9.
For a practical inspection plan, agree on:
1. Sampling: the number of bars or pieces measured from each lot or bundle. 2. Positions: measurements near both ends and at intermediate positions on long bars where required. 3. Orientations: more than one angular reading at a position when roundness or ovality is a concern. 4. Instrument: a calibrated micrometer or other suitable instrument with enough resolution for the tolerance window. 5. Temperature and handling: allow the bar and instrument to reach a suitable inspection condition when close limits make thermal effects relevant. 6. Record identity: show the item, nominal size, tolerance, measured values, date and batch or bundle reference.
The drawing, purchase order or inspection agreement should determine the final sampling plan. A few supplier photos can support the report, but photographs of a micrometer do not replace traceable measured values.
Check straightness, surface and bar ends separately
Diameter is only one part of incoming acceptance. For long stock used in automatic or Swiss-type lathes, inspect straightness using the method agreed with the supplier. A value expressed per meter and a total deviation over full length answer different questions, so the PO should make the basis clear.
Look along the ground surface for longitudinal lines, local burns, chatter marks, handling scratches, rust staining and dents. Not every cosmetic mark affects machining, but a bar supplied for use with little or no skin removal needs a clearer surface criterion than a bar intended for heavy turning.
Ends also deserve attention. Burrs or severely distorted saw cuts can hinder loading and damage packaging. Fixed-length blanks may need a defined cut-length tolerance, while full-length bars need end protection and secure bundling for ocean freight.
Grade choice and traceability
Centerless grinding controls geometry; it does not determine the stainless steel grade. Grade selection still follows the drawing, corrosion exposure, machining route and customer specification.
- 303 stainless steel bar is often considered for repeat machining where sulfur-assisted chip breaking is acceptable under the project specification.
- 304 and 304L serve many general industrial parts, but low-carbon or dual-certified wording must be supported by the actual MTC.
- 316 and 316L add molybdenum for many chloride-sensitive applications, yet the grade does not guarantee performance in every environment.
For every grade, match the heat number on the MTC to the bar or bundle label and packing list. Keep material identity and dimensional acceptance as two separate checks: the MTC supports the first; the measurement report supports the second. The MTC checklist before shipment release explains the document trail in more detail.
FX Stainless Steel maintains 1,000+ tons of stainless steel bar stock across the broader bar range. That figure does not mean every grade, ground diameter or tolerance is immediately available. Ground-bar availability and processing depend on the requested grade, size, length, tolerance, quantity and inspection scope.
RFQ wording example
A useful inquiry gives the supplier enough information to select stock, finishing and inspection routes. For example:
SUS304 centerless ground stainless steel round bar, diameter 20 mm h9 (20.000 / 19.948 mm), 3,000 mm fixed length, 500 kg. Please state straightness, cut-length tolerance, surface roughness and end condition. MTC, heat-number labels and dimensional inspection report required. Standard export packing. Destination: Laem Chabang, Thailand.
Use the example as a structure, not as a universal specification. Replace the grade, limits, straightness, roughness and sampling requirements with values from the actual drawing or machining process.
For a quotation, send these details:
- grade and standard wording;
- nominal diameter and h9 or explicit upper/lower limits;
- straightness, roundness and roughness only where required;
- full length or cut length, including end condition;
- quantity and repeat-order expectation;
- MTC and dimensional-report requirements;
- packing marks and destination country or port.
Common buying mistakes
- Treating “centerless ground” as automatic proof of h9.
- Specifying h9 but omitting the nominal diameter and standard basis.
- Using the MTC as evidence of dimensional tolerance.
- Leaving straightness undefined for a bar-fed CNC job.
- Asking for a roughness value without saying whether it applies before or after the customer’s machining.
- Measuring one point and assuming the full bar has the same diameter and form.
- Paying for ground stock when the first operation removes substantial material.
- Mixing heat numbers or bundle labels so measured pieces cannot be traced to the shipped lot.
Sources and scope
The h9 explanation and the 20 mm example follow ISO 286-2:2010, Geometrical product specifications (GPS) - ISO code system for tolerances on linear sizes - Part 2: Tables of standard tolerance classes and limit deviations for holes and shafts. ISO 286-1:2010 provides the basis of the code system.
This article does not reproduce the full standard and does not set a universal inspection plan. Use the edition, drawing, PO and customer-specific acceptance criteria named by the order.
Conclusion
Centerless ground stainless steel bar earns its cost when controlled starting stock reduces a real machining or acceptance risk. The purchase decision should begin with the part and machine: required diameter window, remaining allowance, feeding condition, straightness, surface and inspection evidence.
Write those requirements into the RFQ and PO. Before release, connect the dimensional report to the correct bundle, then match its heat number with the MTC and packing list. That gives the buyer evidence for both geometry and material identity.
Frequently asked questions
Q. When should I order centerless ground stainless steel bar?
A. Order centerless ground bar when the starting stock needs controlled diameter, a smooth cylindrical surface or stable feeding for shafts, pins, guide bushes and repeat CNC parts. If the first operation removes substantial material, cold-drawn or peeled bar may be more economical.
Q. Does centerless ground stainless steel bar automatically meet h9 tolerance?
A. No. Centerless ground describes a finishing process, not an automatic tolerance guarantee. State the nominal diameter and h9 limits on the drawing or purchase order, then require a dimensional inspection record for the ordered batch.
Q. Does h9 control roundness, straightness and surface roughness?
A. No. h9 controls the permitted size range for the specified external dimension. Roundness, straightness, cylindricity, surface roughness, cut length and end condition need separate limits when they affect the part or bar feeder.
Q. What documents should come with precision ground stainless steel bar?
A. Ask for the MTC and heat-number traceability for material identity, plus a separate dimensional inspection record for diameter and any agreed straightness, roundness or roughness results. The heat number should match the bundle labels and packing list.
Q. What should I include in a centerless ground bar RFQ?
A. State the grade and standard, nominal diameter, tolerance or explicit limits, straightness and roughness if critical, length, end condition, quantity, inspection record, MTC requirement, packing and destination. Include the drawing when the bar will serve as a near-finished shaft or pin.
Request a ground bar quotation
Send the grade, nominal diameter, tolerance limits, length, quantity, inspection requirements and destination through the contact page. We will check the available stock or processing route, dimensional-report requirements, MTC traceability and export packing before quotation.